Have you ever squeezed toothpaste from a tube and watched it emerge in that perfect, consistent ribbon? That simple action captures the essence of one of manufacturing's most versatile processes. When we define aluminum extrusion, we're describing a remarkably similar principle applied at industrial scale with heated metal instead of paste.
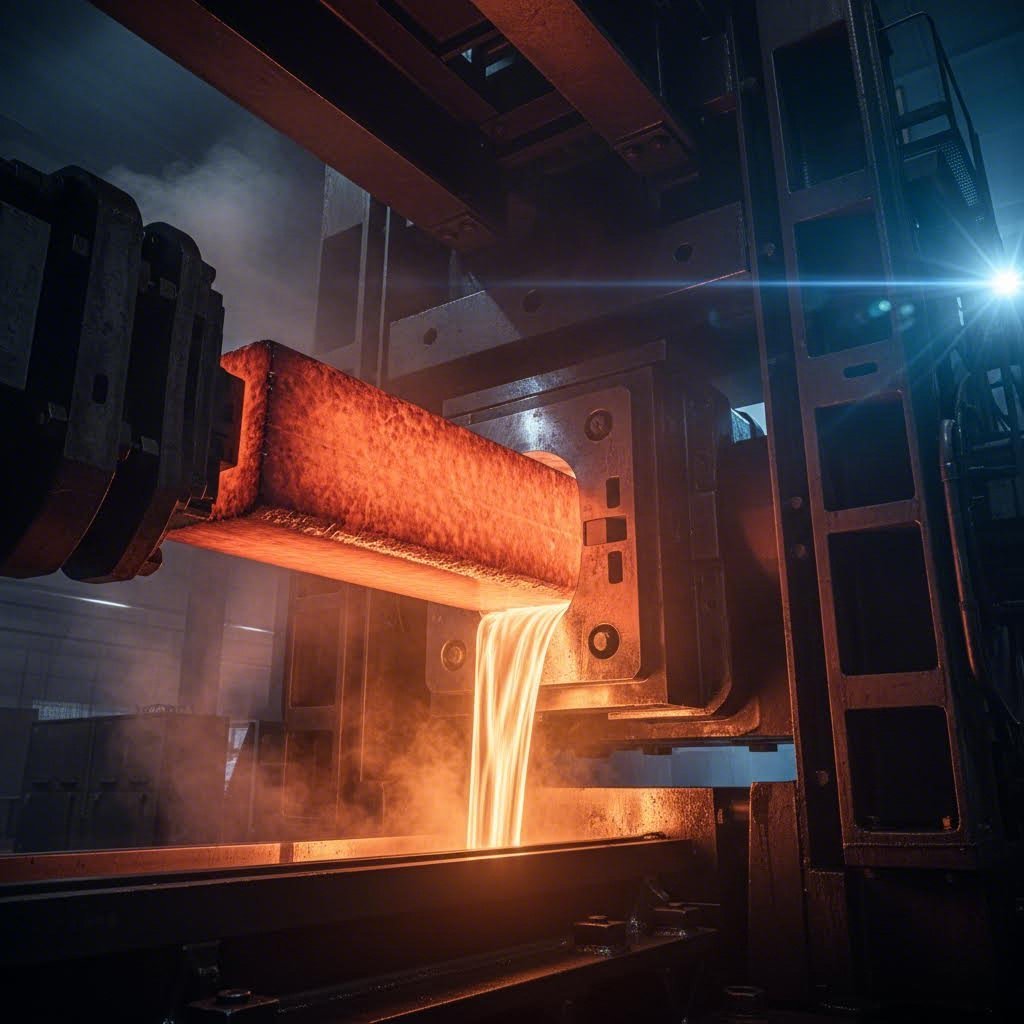
Aluminum extrusion is a fabrication process that forces a heated aluminum billet through a custom-shaped steel die to produce a continuous profile with a consistent cross-section.
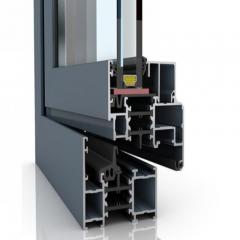
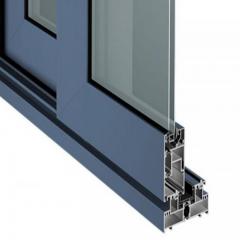
So, what is aluminum extrusion in practical terms? Imagine taking a solid cylindrical log of aluminum, heating it until it becomes soft and pliable, then pushing it through a specially designed opening. The metal flows through that opening and emerges on the other side as a perfectly shaped profile—ready to become window frames, structural beams, heat sinks, or countless other products we encounter daily.
The magic happens when a heated aluminum billet meets the extrusion die. Picture this: a powerful hydraulic ram applies immense pressure—often reaching up to 15,000 tons—forcing the softened metal through the die's precise opening. The aluminum flows like thick honey, conforming exactly to the die's shape.
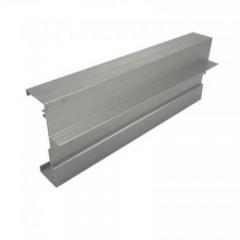
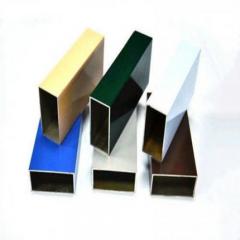
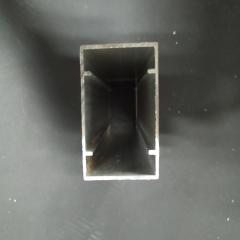
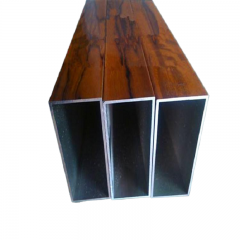
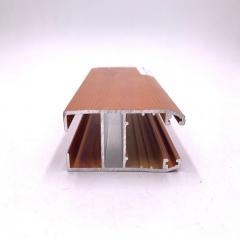
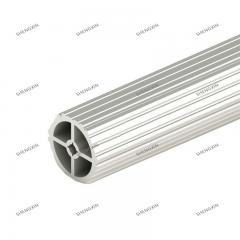
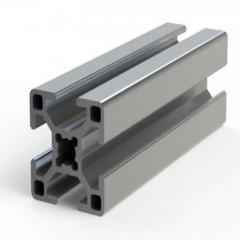
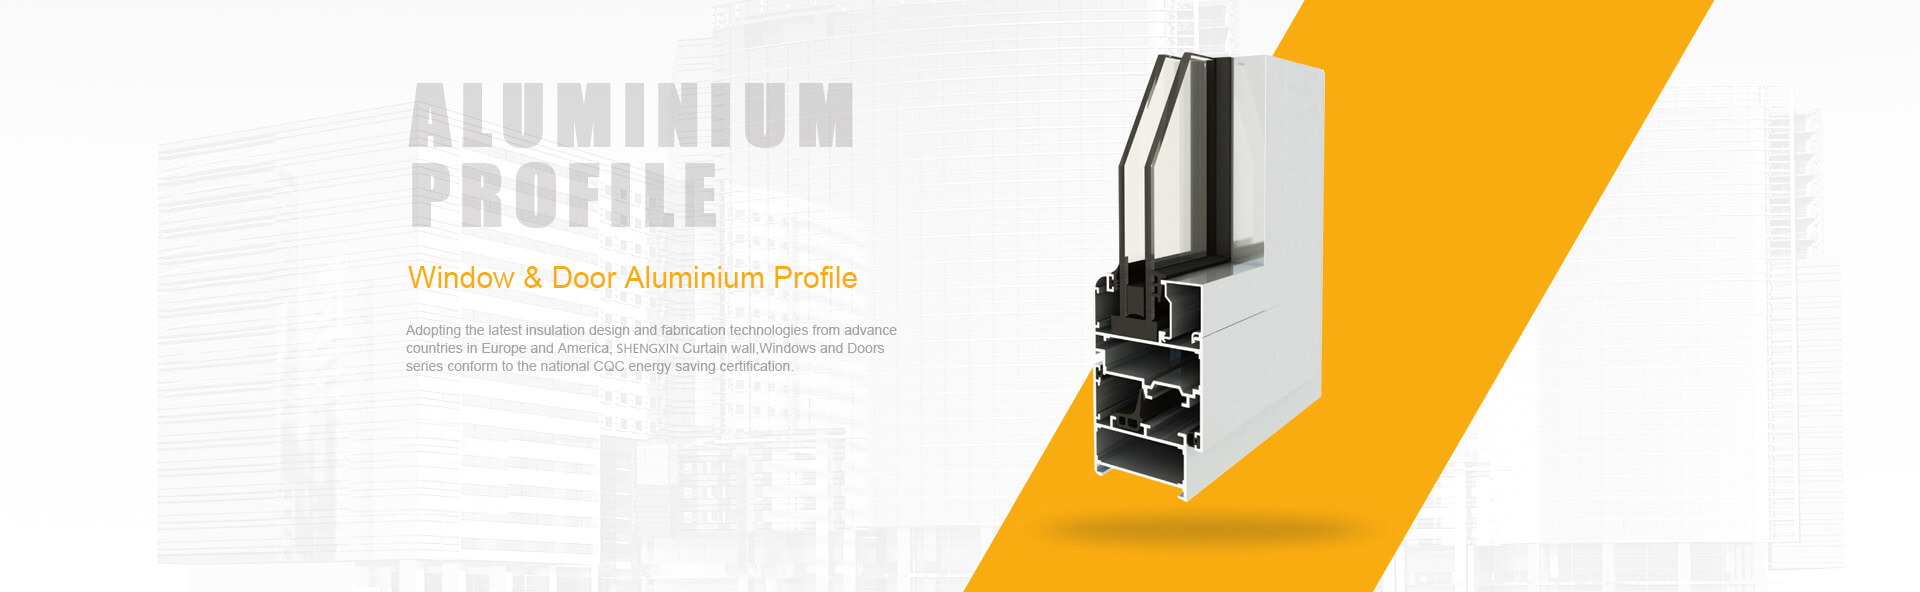
What is extruded aluminum once it emerges? It's a continuous length of material with a uniform cross-section that matches the die perfectly. These profiles can be solid, hollow, or semi-hollow, ranging from simple angles to incredibly complex architectural shapes. The aluminium extrusion definition encompasses this entire transformation—from raw billet to finished profile with exact dimensional accuracy.
You'll find extruded aluminum profiles everywhere once you start looking. The construction industry relies on them for curtain walls and window systems. Automotive manufacturers use them to reduce vehicle weight. Electronics companies depend on extruded heat sinks to keep devices cool.
What is an aluminum extrusion's greatest advantage? It delivers exceptional strength-to-weight ratios while allowing designers tremendous creative freedom. Complex shapes that would be impossible or prohibitively expensive to machine from solid stock become economical through this process. Profiles typically emerge in lengths of 8 to 24 feet, ready for heat treatment, surface finishing, and fabrication to meet exact specifications.
This versatility explains why understanding the extrusion of aluminum alloys matters—whether you're an engineer designing components, an architect specifying materials, or simply curious about how everyday products are made.
Now that you understand how the extrusion process transforms heated billets into precise profiles, here's a critical question: does the type of aluminum alloy matter? Absolutely. Choosing the right aluminum extrusion alloys determines everything from production efficiency to final product performance. Think of it like selecting the right ingredient for a recipe—the wrong choice can undermine even the best process.
Not all aluminum alloys behave the same way when pushed through an extrusion die. Some flow smoothly at lower pressures, producing excellent surface finishes. Others resist deformation, requiring higher temperatures and slower speeds that stress tooling and reduce productivity. Understanding these differences helps you match alloy properties to your specific application demands.
The following table compares the major aluminum alloy extrusion series you'll encounter when specifying extruded aluminum alloy profiles:
| Alloy Series | Extrudability Rating | Typical Applications | Strength Characteristics | Corrosion Resistance |
|---|---|---|---|---|
| 2xxx (Al-Cu) | Poor to Fair | Aerospace structural components, aircraft skins | High tensile strength, excellent fatigue resistance | Poor (requires protective coating) |
| 6xxx (Al-Mg-Si) | Excellent | Architectural frames, automotive parts, general structural | Medium to high strength, good formability | Excellent |
| 7xxx (Al-Zn) | Fair to Good | Aerospace frames, high-stress structural parts | Very high strength, comparable to steel | Moderate (some alloys require protection) |
Why do 6063 and 6061 dominate the types of aluminum extrusion you'll find in most applications? It comes down to a near-perfect balance of properties that make production efficient and results reliable.
Alloy 6063, often called "architectural aluminum," flows through dies like butter. Its magnesium and silicon content creates a material that extrudes at relatively low temperatures and pressures, producing profiles with smooth, attractive surfaces ideal for anodizing. You'll find 6063 in window frames, door systems, and decorative trim where appearance matters as much as function.
Alloy 6061 steps up the strength while maintaining good extrudability. It's the workhorse for structural applications—think machine frames, automotive components, and industrial equipment. While slightly more challenging to extrude than 6063, it rewards manufacturers with profiles that handle higher loads without sacrificing too much production efficiency.
From a production standpoint, these 6xxx alloys extend die life significantly compared to harder alloys. They generate less friction during extrusion, reducing wear on expensive tooling. Faster extrusion speeds translate directly to lower per-part costs—a crucial consideration for high-volume production.
Sometimes standard 6xxx alloys simply won't deliver the performance your application requires. That's where aluminium alloy extrusion gets interesting—and more challenging.
Consider 7075 aluminum extrusion for aerospace and defense applications. This zinc-alloyed material delivers tensile strength approaching that of many steels, making it essential for highly stressed aerospace parts. However, 7075 extrusion demands careful process control. The alloy requires higher billet temperatures, slower ram speeds, and more robust die designs. Die life decreases noticeably, and surface quality requires extra attention during finishing.
The 2xxx series, particularly alloy 2024, earns its place in aerospace for exceptional fatigue resistance—critical for components experiencing repeated stress cycles. These copper-alloyed materials present significant extrusion challenges, including hot shortness (cracking during extrusion) and poor corrosion resistance that demands protective treatments after fabrication.
When selecting an extruded aluminum alloy, consider these key factors:
The right alloy selection balances these considerations against production realities. A profile that looks perfect on paper but destroys dies or requires excessive rework quickly becomes uneconomical. That's why experienced extruders often recommend starting with proven 6xxx alloys and moving to specialty materials only when performance demands truly require them.
With the right alloy selected for your application, the next critical factor becomes process execution—how temperature, pressure, and speed work together to transform your chosen material into flawless profiles.
Ever wondered how aluminum extrusion is made from start to finish? The transformation from a simple cylindrical billet to a precision-engineered profile involves a carefully orchestrated sequence of steps—each one critical to the final product's quality. Understanding how does aluminum extrusion work gives you insight into why certain design choices matter and how process parameters affect your finished parts.
The aluminum extrusion process combines intense heat, tremendous pressure, and precise timing. Get any variable wrong, and you'll face defects ranging from surface blemishes to structural failures. Get them right, and you'll produce profiles with exceptional dimensional accuracy and mechanical properties.
Here's exactly how extruded aluminum is made, broken down into the essential stages that every billet must complete:
The final step? Aging. Cut profiles load onto transport racks and enter age ovens where controlled heat treatment—artificial aging—develops the metal's ultimate mechanical properties. This entire extrusion aluminium process, from heated billet to aged profile, can take as little as a few hours for simple shapes.
If there's one variable that separates excellent extrusions from problematic ones, it's temperature. As industry experts note, temperature is the most critical factor because it directly determines aluminum's characteristics—hardness, surface finish, and dimensional accuracy all depend on maintaining precise thermal control throughout the aluminium extrusion process.
Why does temperature matter so much? Consider what happens at the extremes:
The solution? Isothermal extrusion—a process control approach that maintains consistent temperature throughout the extrusion cycle. According to research from 3T True Temperature Technologies, achieving isothermal conditions requires accurate temperature measurement with tolerances of ±5°C (10°F) along the billet axis, plus precise monitoring of die exit temperatures.
Modern extrusion presses use True Temperature Technology (3T) instruments mounted on the press platen to record exit temperatures in real-time. This data enables operators to maintain maximum press speeds while staying within the metallurgical sweet spot for each alloy. The goal is reaching solution heat-treat temperatures—typically 930-980°F for 6000 series alloys—right at the die exit to develop optimum mechanical properties.
Taper heating adds another layer of sophistication. Rather than heating billets uniformly, modern systems create a temperature gradient along the billet's length. This compensates for the frictional heat generated as the billet moves through the container, helping maintain consistent exit temperatures from start to finish.
The relationship between temperature, pressure, and speed creates a delicate balance. Higher temperatures allow faster extrusion but risk surface defects. Lower temperatures improve quality but demand more pressure and slow production. Finding the optimal combination for each alloy and profile shape separates efficient operations from struggling ones.
Understanding how is aluminum extrusion made at this level of detail reveals why the process demands both sophisticated equipment and experienced operators. The next consideration—choosing between direct and indirect extrusion methods—adds another dimension to process optimization.
Now that you understand the step-by-step aluminum extrusion process, here's an important question: does the direction of metal flow actually matter? When selecting extrusion manufacturing methods, engineers face a fundamental choice between two approaches—each with distinct advantages that can significantly impact your final product quality and production economics.
Think of it this way: both methods accomplish the same goal of forcing heated aluminum through a shaped die. But how they accomplish this creates meaningful differences in friction, surface finish, and material utilization that smart specifiers leverage to their advantage.
| Characteristic | Direct Extrusion | Indirect Extrusion |
|---|---|---|
| Friction Characteristics | High friction between billet and container walls | Significantly reduced friction—material doesn't slide against container |
| Surface Quality | Good, but may show more variation | Superior—smoother, more consistent finish |
| Billet Utilization | Lower—more material lost to discard | Higher—less waste, better material efficiency |
| Equipment Complexity | Simpler design, easier maintenance | More complex machinery, higher setup costs |
| Ideal Applications | Large cross-sections, simple profiles, high-volume production | Precision parts, complex shapes, superior surface requirements |
In direct extrusion, the ram pushes the heated billet forward through a stationary die—just like squeezing that tube of toothpaste we mentioned earlier. The material and ram move in the same direction, with aluminum flowing directly toward and through the die opening.
Why does this method dominate metal extrusion operations worldwide? Several practical advantages explain its popularity:
The tradeoff? As the billet moves through the container, it generates substantial friction against the container walls. This friction demands higher pressure, accelerates die wear, and can create uneven material flow—particularly toward the end of each push when the remaining billet must overcome accumulated frictional resistance.
Despite these challenges, direct extrusion remains the industry standard for most applications. The cost-effectiveness and operational familiarity simply outweigh the friction-related drawbacks for typical production scenarios.
Indirect extrusion flips the conventional approach. Here, the die mounts on a hollow ram that moves toward the billet, which remains stationary within the container. Sounds complex? Imagine pushing a cookie cutter into dough rather than pushing dough through a cutter—the result is similar, but the mechanics differ significantly.
This reversed arrangement eliminates the friction between billet and container walls because the aluminum doesn't actually slide along those surfaces. The benefits cascade from there:
So why isn't everyone using indirect extrusion? The equipment complexity and associated costs limit its adoption. The hollow ram design is more difficult to manufacture and maintain. Additionally, indirect presses typically handle smaller profile sizes than their direct counterparts, restricting their application range.
Industries demanding the highest precision—aerospace, electronics, and specialized automotive components—often find indirect extrusion worth the investment. When surface quality and dimensional consistency justify premium processing costs, this method delivers results that direct extrusion simply cannot match.
Beyond these two primary approaches, hydrostatic extrusion represents an emerging variation worth monitoring. This technique surrounds the billet with pressurized fluid, eliminating direct contact between metal and container entirely. While still relatively uncommon in aluminum processing, hydrostatic methods show promise for extremely difficult-to-extrude alloys and ultra-precise applications where conventional direct indirect extrusion approaches fall short.
Understanding which extrusion method suits your application helps you make informed decisions when specifying profiles. But regardless of which approach produces your parts, the die itself determines what shapes are possible—making die design principles the next essential topic to master.
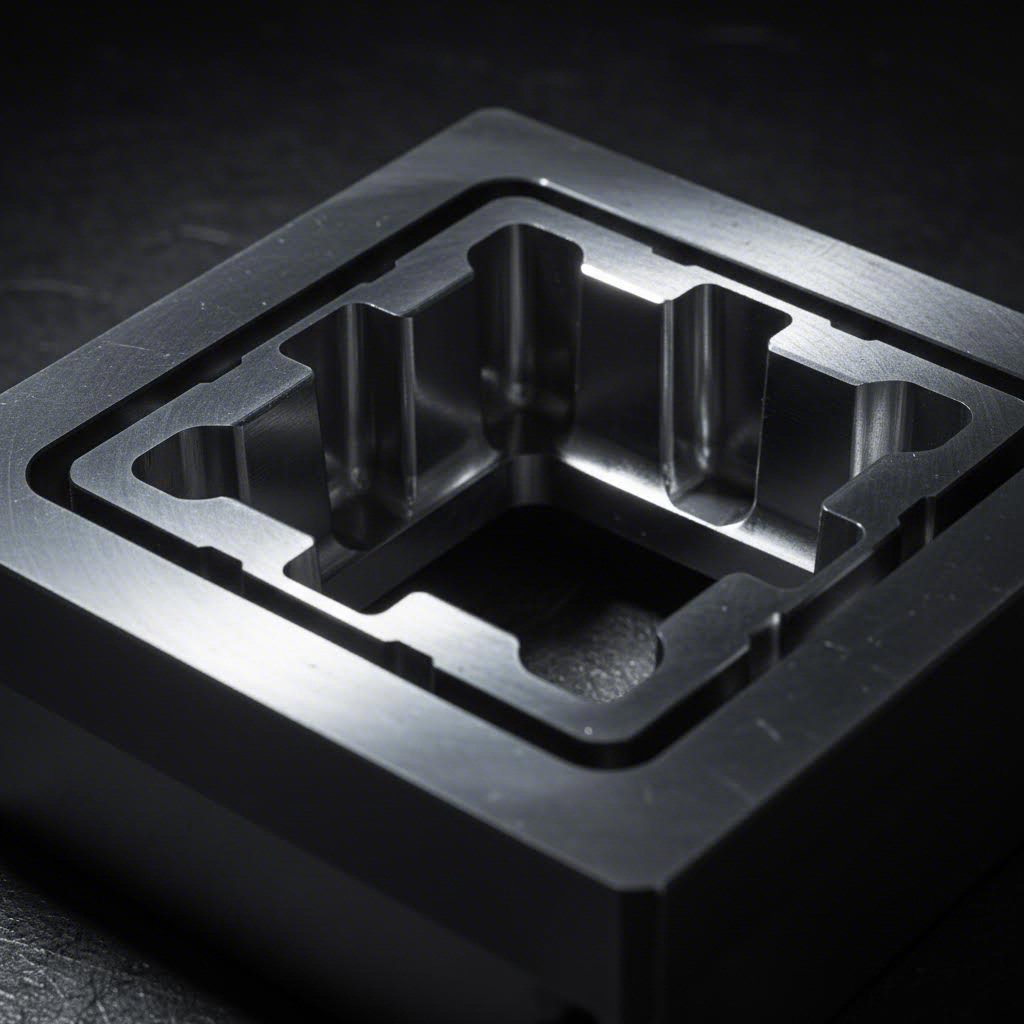
You've selected your alloy, optimized your process parameters, and chosen between direct and indirect extrusion. But here's the reality: none of that matters if your aluminum extrusion die isn't engineered correctly. The die is where theory meets metal—literally. It's the precision-machined steel component that transforms a heated billet into the exact profile your application demands.
Think of die design as the hidden art behind every successful extrusion operation. A well-designed aluminum extrusion die produces thousands of feet of flawless profile with minimal wear. A poorly conceived one creates headaches from the first push—dimensional inconsistencies, surface defects, and premature tooling failure that send production costs spiraling.
The type of aluminum extrusion dies you need depends entirely on your profile geometry. Simple solid shapes like bars, angles, and channels use flat-face or solid dies—relatively straightforward tooling where aluminum flows directly through a shaped opening in a single steel plate.
Hollow sections? That's where die design gets interesting. Creating internal cavities requires porthole dies (also called bridge dies), which split the aluminum flow around solid supports before reuniting it in a welding chamber. Imagine the metal dividing to flow around obstacles, then rejoining seamlessly before exiting the die opening.
According to research published in Metals journal, porthole dies for complex profiles like heatsinks with large wall thickness variations present particular challenges. The study found that achieving uniform metal flow velocity is the most important factor for improving extrusion quality and extending die life. When wall thickness varies dramatically—say, from 1.5mm fins to 23mm base sections—metal naturally wants to flow faster through thicker areas, creating distortion and dimensional defects.
Semi-hollow dies bridge the gap between these extremes. They're used when profiles have partially enclosed voids—shapes where the tongue ratio (the ratio of void depth to opening width) falls within specific limits. These aluminium extrusion dies combine elements of both solid and hollow designs, offering versatility for complex geometries.
Successful profile extrusion of hollow sections depends on several critical design elements:
Here's a question that matters to your bottom line: how do aluminium extrusion tooling choices affect what you'll actually pay for parts?
Bearing length optimization represents one of the most powerful tools in a die designer's arsenal. The bearing is the parallel land at the die exit where aluminum makes final contact before emerging as a finished profile. Longer bearings slow metal flow by increasing friction; shorter bearings allow faster exit speeds. By varying bearing lengths across the die opening, designers control exactly how fast each portion of the profile exits—essential for preventing the bowing and twisting that occurs when different sections exit at different velocities.
Research demonstrates the effectiveness of this approach. In one study, adjusting bearing lengths reduced the velocity relative difference (VRD) from 4.1% to just 0.75%, virtually eliminating geometric defects in a complex heatsink profile. The general rule? Increase bearing length where metal flows too fast; reduce it where flow lags.
Pocket design provides another flow-control mechanism. Pockets—recessed areas ahead of the die opening—act as secondary welding chambers that redistribute metal before it enters the bearing zone. For complex profiles with significant wall thickness variation, modifying pocket geometry can dramatically improve flow balance, reducing velocity differences from 2.09 mm/s to just 0.89 mm/s in documented cases.
Die correction techniques come into play when initial designs don't perform as expected. Even experienced designers often require adjustments after trial extrusions. Common corrections include:
What about die life and maintenance? H13 tool steel remains the standard material for aluminum extrusion dies, offering excellent thermal conductivity, wear resistance, and toughness. Surface treatments like nitriding extend service life by hardening the die surface, while regular inspection catches wear before it affects profile quality.
Die complexity directly drives tooling costs and lead times. A simple solid die might cost a few thousand dollars and arrive in two weeks. Complex hollow dies with multiple portholes, intricate pocket geometries, and tight tolerances can cost ten times more and require months of design iteration and manufacturing. However, as one industry analysis notes, investing in proper die design upfront prevents the expensive cycle of trial-and-error corrections that plague poorly planned tooling programs.
The die represents just one piece of the aluminium extrusion tooling puzzle. Support tooling—backer plates, bolsters, and sub-bolsters—must withstand pressures up to 15,000 tons while maintaining perfect alignment. Extrusion press tooling including stems, dummy blocks, and containers completes the system. Every component must work in harmony for consistent results.
With properly designed dies producing quality profiles, the next phase of the journey begins: post-extrusion processing that transforms raw extrusions into finished components ready for assembly.
Your aluminum profile has emerged from the die, cooled on the run-out table, and been cut to length. But here's what many people don't realize: the extrusion itself is often just the beginning. What happens next—heat treatment, surface finishing, and secondary fabrication—transforms raw extruded aluminum into components ready for demanding real-world applications.
Think about it this way: an untreated extrusion is like a blank canvas. Post-extrusion processing adds the performance characteristics, protective qualities, and aesthetic appeal that your specific application requires. Understanding these aluminum extrusion processing options helps you specify exactly what you need—and avoid paying for treatments you don't.
Ever noticed designations like T5 or T6 following an alloy number? These aren't random codes—they indicate specific heat treatment processes that dramatically affect how your aluminium extrusion parts will perform under load.
The T5 temper involves cooling the extrusion after it exits the die, then artificially aging it in an oven. This process develops moderate strength improvements without the complexity of full solution heat treatment. You'll find T5 temper ideal for finished extrusions that won't undergo additional forming—window frames, architectural trim, and heat sinks are common examples. Alloy 6063-T5 delivers the perfect balance of strength and surface quality for decorative applications.
Need maximum strength? The T6 temper takes extruded parts through a more intensive process: solution heat treatment by artificial aging. The results speak for themselves:
This significant strength increase comes with a tradeoff—reduced ductility of around 8-10%. What does this mean practically? T6-tempered profiles require careful planning for tight bends to prevent cracking. If your design demands post-treatment forming or welding, consider specifying T4 temper instead, which prioritizes formability over maximum strength.
Here's a critical consideration for welded assemblies: T6 aluminum loses its temper properties in weld zones. The heat-affected area essentially reverts to a softer state, potentially creating weak points in structural applications. Plan for post-weld heat treatment or design around T4/T5 tempers when welding is unavoidable.
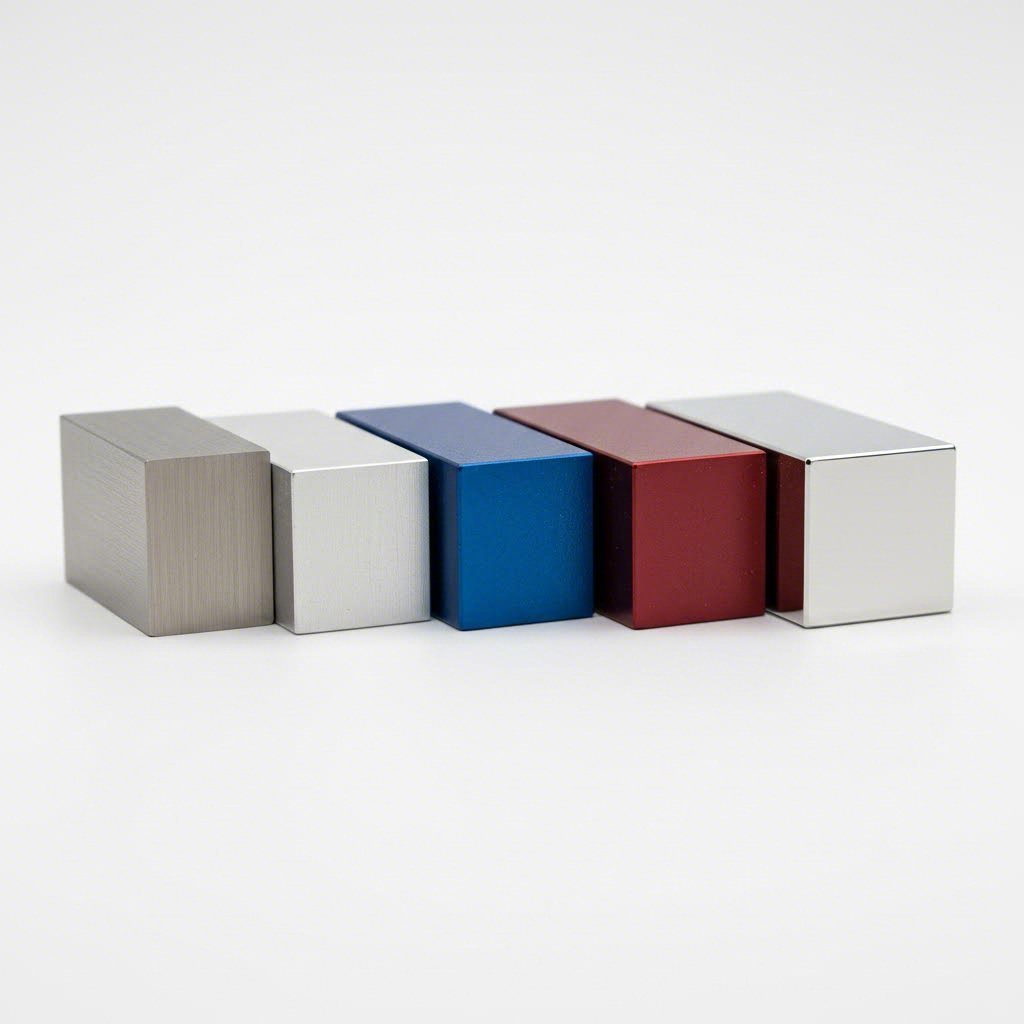
Raw aluminum develops a natural oxide layer that provides basic corrosion protection. But for most applications, you'll want enhanced surface treatments that deliver superior durability, specific colors, or particular aesthetic effects. The surface treatment you choose depends on environmental exposure, visual requirements, and budget considerations.
Quality considerations vary by finishing method. Anodizing requires careful surface preparation—any scratches or handling marks become permanently visible. Powder coating thickness must remain consistent to prevent orange peel texture or coverage gaps. PVDF applications demand precise mil thickness control for warranty compliance.
Beyond protective finishes, surface textures like brushing create distinctive striated patterns for modern architectural aesthetics, while polishing produces mirror-like reflectivity for high-end decorative applications. These mechanical finishes can stand alone or combine with protective treatments for both beauty and durability.
Secondary extrusion fabrication operations transform finished profiles into ready-to-install components. Extruded aluminum CNC machining adds precision features—holes, slots, pockets, and threaded ports—with tolerances impossible to achieve through extrusion alone. Cutting, drilling, and bending operations configure profiles to exact specifications, eliminating field fabrication and ensuring consistent quality across production runs.
For manufacturers seeking comprehensive aluminum processing capabilities, facilities offering integrated deep processing services streamline the path from raw extrusion to finished component. Shengxin Aluminium's processing services exemplify this approach, combining state-of-the-art CNC machining centers with extensive surface treatment options—including custom anodizing colors, powder coating, PVDF, and micro-arc oxidation—all under one roof. This integration eliminates coordination between multiple vendors while ensuring consistent quality from die development through final finishing.
With heat treatment, surface finishing, and secondary fabrication complete, your aluminium extrusion parts are ready for their intended application. But what happens when something goes wrong during the extrusion process itself? Understanding common defects—and how to prevent them—keeps production running smoothly.
Even with optimized alloys, precise temperature control, and well-designed dies, aluminum extrusions can develop defects that compromise quality. Here's the reality: defects affect aesthetics, functionality, and structural integrity of finished products. For manufacturers serving customers with stringent quality requirements, understanding what causes these flaws—and how to eliminate them—separates profitable operations from struggling ones.
The good news? Most defects arise from controllable process variables. By recognizing problems early and implementing targeted corrections, you can maintain consistent quality across production runs while minimizing scrap and rework costs.
| Defect Type | Visual Identification | Root Causes | Corrective Actions |
|---|---|---|---|
| Surface Cracking/Tears | Fine cracks at edges and high-friction zones | Excessive extrusion speed, high exit temperature, poor billet quality | Reduce ram speed, optimize billet temperature, use isothermal extrusion techniques |
| Blistering/Scales | Small raised bubbles or regions on profile surface | Trapped gases below billet surface, moisture contamination, lubricant issues | Implement burp cycles, use machined billets, control storage conditions, consider extruding without lubricant |
| Die Lines | Indented or raised lines running along extrusion length | Worn or damaged die surfaces, aluminum buildup on die, contamination | Regular die cleaning and polishing, apply wear-resistant coatings, replace degraded dies |
| Dimensional Variation | Profile dimensions outside specified tolerances | Non-uniform billet heating, inconsistent metal flow, improper bearing lengths | Implement gradient heating, adjust bearing lengths, optimize pocket design |
| Internal Voids | Hollow areas within profile cross-section (detected via testing) | Incomplete welding in porthole dies, insufficient pressure, improper die design | Increase extrusion pressure, redesign welding chamber geometry, verify die alignment |
Surface scratches rank as the most common defect affecting extruded profiles. According to industry research, these superficial abrasions typically result from contact between aluminum and particles or materials during the extrusion process. Poor handling and insufficient lubrication compound the problem.
What should you look for during inspection? Visual examination reveals most surface issues immediately:
Back-end defects present unique challenges. These annular separations—sometimes called fishtail defects—occur in the rear third of an extrusion when friction between the billet and container causes the material to separate into external and internal zones. Catching these issues requires systematic inspection of each push's trailing section.
Temperature, speed, and die condition form the critical triangle that determines whether your extruded aluminum profiles emerge flawless or flawed. Understanding how these variables interact enables targeted corrections rather than trial-and-error troubleshooting.
Temperature control serves as the foundation. Isothermal extrusion—maintaining consistent temperature throughout each push—prevents many surface defects before they start. This technique involves gradient heating different billet sections to compensate for frictional heat buildup. When each zone feeds through the die at consistent temperature, surface quality improves dramatically.
Extrusion speed directly impacts defect formation. Reducing exit speeds prevents excessive metal deformation that causes aluminum to stick to die surfaces—a primary cause of scratching. Yes, slower speeds reduce output, but liquid nitrogen cooling at the deformation zone enables faster production without sacrificing quality.
Die condition determines whether aluminum extrusion profile surfaces meet specifications. Routine cleaning and polishing after each cycle eliminates minute particles that cause markings. Wear-resistant coatings reduce friction and material adhesion. Maintaining proper hardness through periodic nitriding extends die life while preventing the brittleness that leads to breakages.
For blistering prevention specifically, manufacturers employ several proven techniques: burp cycles that temporarily release ram pressure to allow trapped gases to escape, machined billets that remove surface impurities, and controlled storage conditions that prevent moisture absorption.
Quality control inspection methods ensure defects don't reach customers. Leading manufacturers implement comprehensive inspection protocols including:
Statistical process control transforms reactive troubleshooting into proactive quality management. By continuously monitoring billet temperature, ram speed, exit temperature, and cooling rates, operators identify deviations before they affect finished products. Real-time data enables immediate corrections—preventing entire production runs from falling outside specifications.
Documentation and traceability complete the quality system. Material certifications stating actual chemical composition, production specifications, and lot numbers traceable back to raw billet production provide accountability and enable root cause analysis when issues arise.
With defects understood and controlled, the next question becomes: where do all these carefully produced aluminum extrusions actually end up? The applications span virtually every industry—from the buildings you enter to the vehicles you drive.
So what are aluminum extrusions actually used for once they've been processed, treated, and finished? The answer might surprise you with its breadth. From the window frame in your office to the battery enclosure in the latest electric vehicle, extruded aluminium shapes modern life in ways most people never notice.
Understanding these aluminum extrusion applications helps you connect the technical knowledge covered earlier—alloy selection, process parameters, die design—to real-world outcomes. Each industry demands specific combinations of strength, corrosion resistance, surface finish, and dimensional precision that drive material and process decisions.
The building and construction sector remains the dominant consumer of extruded aluminum profiles, accounting for over 50% of global demand. Walk through any modern commercial building, and you're surrounded by types of extruded aluminum working quietly in the background.
Design considerations for architectural applications prioritize surface finish quality—any visible scratches or die lines become permanent once anodized. Symmetrical cross-sections cool more uniformly, reducing distortion. And thermal break profiles require precise tongue-and-groove geometries that demand sophisticated porthole die designs.
Beyond buildings, high-performance aluminum extrusions serve industrial applications where function trumps aesthetics. Here, alloy selection shifts toward strength and thermal properties rather than surface appearance.
Transportation applications showcase aluminum's weight-saving potential. Automotive manufacturers increasingly specify extruded profiles for battery enclosures, side-impact pillars, and underbody structures in electric vehicles. The average extrusion content per EV is projected to reach 80 kg by 2030—up significantly from traditional vehicles. Rail components, including interior framing and exterior body sections, benefit similarly from aluminum's strength-to-weight advantage.
Renewable energy represents one of the fastest-growing aluminum extrusion applications. Solar mounting systems—both rooftop and utility-scale—rely heavily on corrosion-resistant extruded frames and support structures. These project-ready components must withstand decades of outdoor exposure while maintaining structural integrity under wind and snow loads.
Consumer products round out the application spectrum: bicycle frames, furniture components, sporting goods, and countless household items leverage extruded aluminum's versatility. Profile complexity here ranges from simple tubes to intricate decorative shapes that showcase the extrusion process's creative potential.
What's clear across all these sectors? The specific combination of alloy, temper, surface treatment, and profile geometry must match application demands precisely. Understanding how these variables interact—the knowledge you've built through the preceding sections—enables informed specification decisions that balance performance, manufacturability, and cost.
But how do you translate application requirements into manufacturable designs? The next section provides practical guidelines that ensure your profiles can actually be produced efficiently and economically.
You've learned about alloys, processes, dies, and finishing options. Now comes the practical question every engineer faces: how do you design an aluminum extrusion profile that actually works—both technically and economically? The gap between a concept sketch and a manufacturable part often determines project success or failure.
Here's the reality: minor design adjustments can dramatically impact production costs, die life, and final part quality. Following an aluminum extrusion design guide isn't about limiting creativity—it's about channeling innovation into shapes that extrude efficiently while meeting your performance requirements.
The guidelines below represent accumulated industry wisdom. They'll help you avoid the frustrating cycle of design revisions that plague projects where manufacturability wasn't considered upfront.
Why does wall thickness matter so much? Think about what happens inside the die: aluminum extrusion material flows like thick honey through available openings. Thin sections restrict flow, requiring higher pressure. Thick sections allow easy passage, potentially starving adjacent thin areas.
According to Aluminum Extruders Council guidelines, balanced walls rank among the most critical design practices. When your profile absolutely requires thickness variations, use smooth transitions rather than abrupt steps. Tapered sections guide metal flow gradually, preventing the turbulence and separation that cause surface defects.
What about hollow sections? Cavity aspect ratios should stay within 1:3—meaning the void depth shouldn't exceed three times the opening width. Industry research indicates that rounded corners may allow extending to 1:4, but overly deep or narrow voids cause metal flow stagnation or cracking.
Ribs and stiffeners deserve strategic placement. These features improve profile rigidity and minimize post-extrusion warpage. When positioned thoughtfully, they also equalize flow paths inside the die—reducing press load imbalance and improving overall production efficiency.
Every design decision ripples through production economics. Understanding these connections helps you make informed tradeoffs between ideal geometry and practical constraints.
The circumscribing circle diameter (CCD)—the smallest circle that completely encloses your profile's cross-section—directly determines which presses can produce your part. Most economical profiles fit within a CCD between one and ten inches, with dimensions below 8 inches reducing costs significantly. Why? Smaller CCDs require less extrusion force, allowing production on more widely available press sizes.
Consider press availability when sizing your design. Facilities with diverse press capacities—ranging from smaller 600-ton units to larger 5500-ton machines—can accommodate various profile sizes. However, the sweet spot for cost-effective production typically falls within that sub-8-inch CCD range. Larger profiles limit your supplier options and often command premium pricing.
Weight-per-foot affects profitable press operation as much as CCD. As one aluminium extrusion design guide notes, profiles are most enhanced economically when CCD stays under 8 inches and weight remains at 3 pounds per foot or less. Heavier profiles require slower extrusion speeds and more robust tooling.
Die complexity drives tooling costs directly. Simple solid dies might cost a few thousand dollars; complex porthole dies with multiple flow channels can reach ten times that investment. Consider these cost-impacting factors:
The die difficulty ratio—profile area divided by perimeter—quantifies how challenging your design is to extrude. Higher ratios indicate simpler geometry; lower ratios signal complexity that may require design simplification.
Early collaboration between designers, die manufacturers, and extrusion plants prevents costly rework. By discussing manufacturability constraints during the design phase, projects achieve shorter lead times and avoid the expensive trial-and-error corrections that plague poorly planned tooling programs.
For engineers requiring comprehensive support from concept through production, partnering with vertically integrated manufacturers offers significant advantages. Shengxin Aluminium's capabilities—including 35 extrusion presses ranging from 600T to 5500T, in-house die development, and complete deep processing services—enable design optimization that considers die feasibility, press selection, and downstream fabrication simultaneously. This integrated approach transforms aluminium extrusion design guidelines from abstract principles into practical, cost-optimized solutions.
Remember: the goal isn't minimizing design ambition—it's maximizing value within production realities. Profiles that look perfect on paper but destroy dies or require excessive rework quickly become uneconomical. By applying these extrusion profiles design principles from the start, you'll create parts that deliver performance, appearance, and cost-effectiveness in equal measure.
Aluminum extrusion involves heating cylindrical billets to 800-925°F, then forcing the softened metal through a precision steel die using hydraulic pressure up to 15,000 tons. The aluminum emerges as a continuous profile matching the die's cross-sectional shape. The process includes ten critical stages: billet heating, die preheating, billet loading, transfer to cradle, pressure application, material flow through die, profile emergence, cooling/quenching, stretching for straightening, and cutting to length. Finally, profiles undergo artificial aging to develop optimal mechanical properties.
The 6xxx series alloys dominate aluminum extrusion applications. Alloy 6063, called 'architectural aluminum,' offers excellent extrudability, smooth surface finishes ideal for anodizing, and superior corrosion resistance—perfect for window frames and decorative trim. Alloy 6061 provides higher strength while maintaining good extrudability, making it the workhorse for structural applications like machine frames and automotive components. For aerospace requiring maximum strength, 7075 aluminum delivers tensile strength comparable to steel, though it demands more challenging process control and specialized die designs.
Common extrusion defects include surface cracking from excessive speed or temperature, blistering caused by trapped gases or moisture contamination, die lines from worn tooling, dimensional variations due to non-uniform heating, and internal voids from incomplete welding in hollow profiles. Prevention requires isothermal extrusion techniques, proper temperature control, regular die maintenance, optimized bearing lengths, and statistical process control monitoring. Quality inspection methods include dimensional checks with CMM equipment, visual surface examination, and mechanical testing for strength verification.
In direct extrusion, a ram pushes the heated billet through a stationary die—the most common method offering simpler equipment and lower costs. Indirect extrusion moves the die toward a stationary billet, eliminating friction between billet and container walls. This friction reduction in indirect extrusion results in lower pressure requirements, superior surface finish, better dimensional consistency, and extended die life. However, indirect extrusion requires more complex equipment and typically handles smaller profile sizes, making it ideal for precision aerospace and electronics applications.
Extruded aluminum serves diverse industries. Architectural applications—window frames, curtain walls, and structural glazing—account for over 50% of global demand. Transportation uses include automotive battery enclosures, vehicle frames, and rail components, with EV extrusion content projected to reach 80 kg per vehicle by 2030. Industrial applications encompass T-slot machine frames, conveyor systems, and heat sinks for electronics cooling. Renewable energy relies on extruded mounting systems for solar installations. Consumer products including bicycle frames, furniture, and sporting goods also leverage aluminum extrusion's versatility and strength-to-weight advantages.


 Onlineservice
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 Deutsch
 English
 français
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська