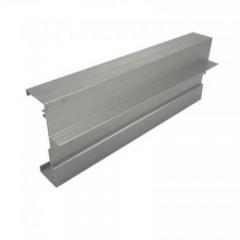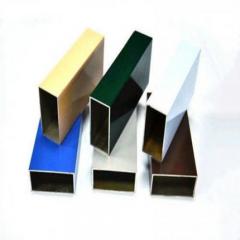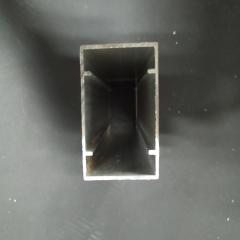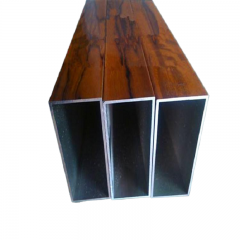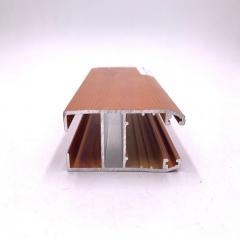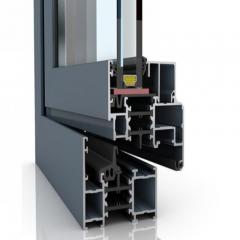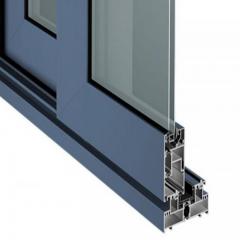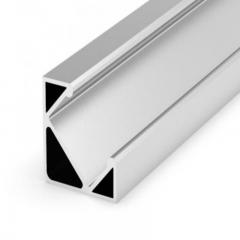
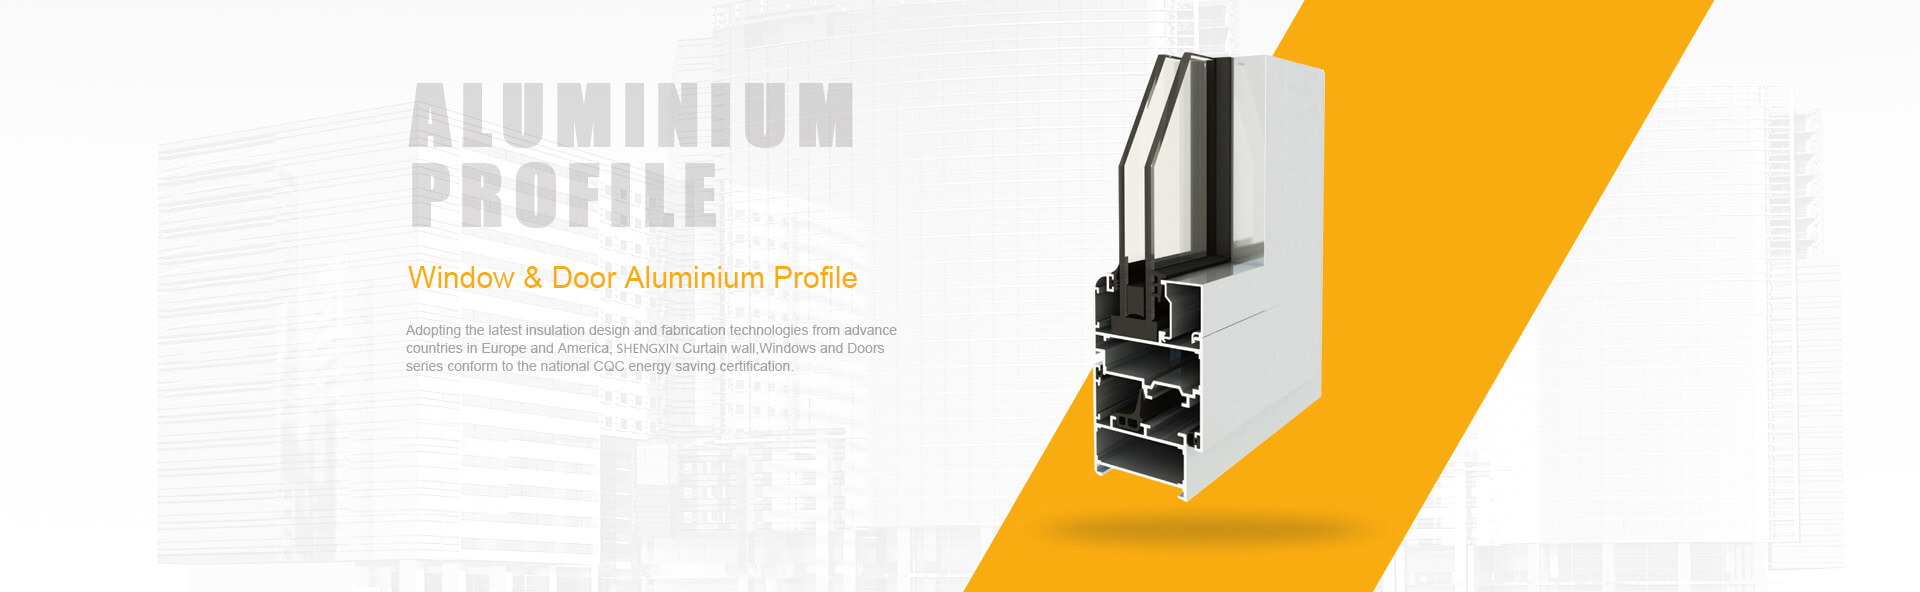
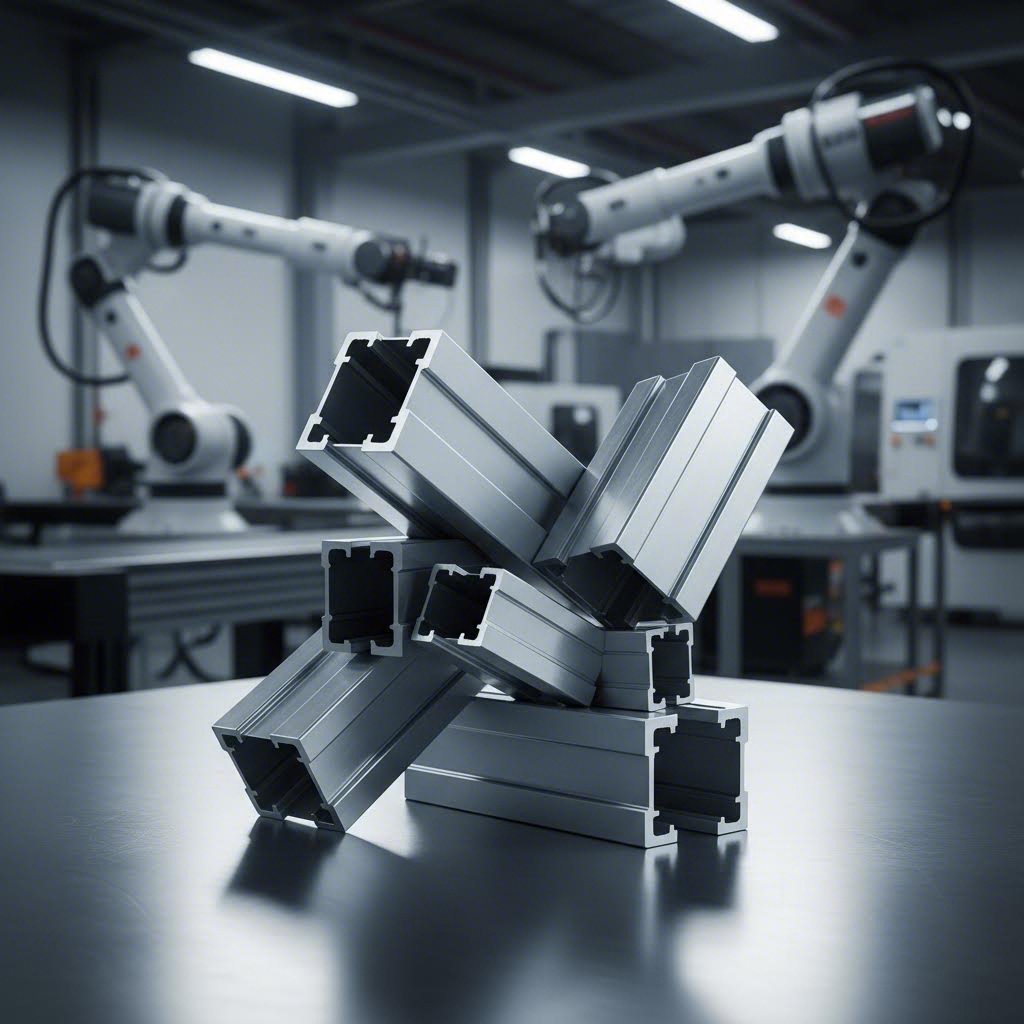
Ever wondered how those perfectly uniform aluminum channels in window frames or industrial equipment get their precise shapes? The answer lies in a fascinating manufacturing process that transforms raw aluminum into incredibly consistent profiles. An aluminum extrusion channel is a structural component created by forcing heated aluminum through a specially designed die, producing continuous lengths with uniform cross-sections. Whether you're an engineer specifying materials or a DIY enthusiast tackling your first project, understanding this process helps you make smarter decisions.
Think of extrusion like squeezing toothpaste through a shaped opening. The aluminum extruded through a die emerges in the exact profile of that opening, maintaining its shape along the entire length. This process starts with a cylindrical aluminum billet, which is preheated to approximately 800-925°F. At this temperature, the metal becomes malleable without melting, allowing it to flow smoothly through the die.
What makes extruded aluminum channel so reliable? The secret lies in the controlled conditions of the process. A hydraulic ram applies tremendous pressure—often reaching 15,000 tons—to push the softened billet through the die opening. This force ensures the aluminum completely fills every contour of the die, creating aluminum channel extrusions with exceptional dimensional accuracy.
Unlike rolled or formed alternatives that bend flat sheets into shape, extrusion forces material through a single die in one continuous motion, eliminating the inconsistencies that arise from multiple forming stages and producing profiles with superior dimensional uniformity throughout their entire length.
The journey from raw aluminum to finished extruded aluminum channel follows a carefully orchestrated sequence. First, manufacturers preheat the steel die to around 750-900°F to ensure optimal metal flow and extend the die's service life. The prepared billet then enters the press, where lubricant prevents it from sticking to the ram during extrusion.
Once the profile emerges from the die, it undergoes rapid cooling through water baths or forced air—a process called quenching. This step locks in the mechanical properties of the metal. Workers then stretch the profiles to correct any minor twisting and achieve proper alignment. Finally, the extruded aluminium channel is cut to standard or custom lengths and may receive additional heat treatment to reach specific temper grades like T5 or T6.
How does this compare to roll forming? While roll forming passes metal through a series of rollers to gradually shape it, extrusion achieves the final profile in a single pass. Roll forming works well for simpler shapes and very high volumes, but extrusion excels at creating complex cross-sections with tighter tolerances and lower tooling costs for moderate production runs. For projects requiring precise wall thickness control and intricate geometries, the extrusion process delivers consistency that other methods simply cannot match.
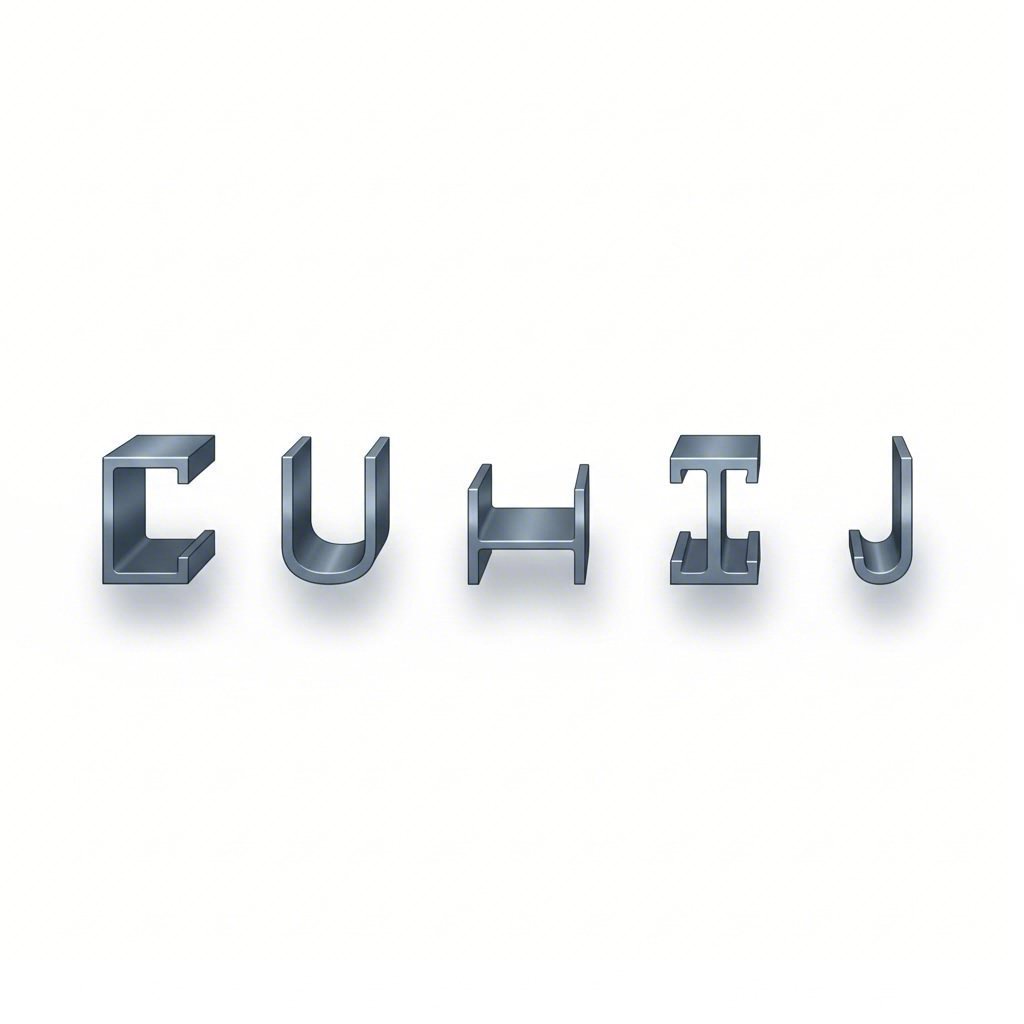
Now that you understand how these profiles are manufactured, the next question becomes: which shape works best for your application? With so many aluminium channel types available, selecting the right profile can feel overwhelming. Each design serves distinct purposes, and choosing incorrectly can mean compromised performance or unnecessary costs. Let's break down the most common profiles you'll encounter and explore exactly when to use each one.
These two profiles often get confused because they look similar at first glance. However, their structural differences make each suited to very different applications.
An aluminum c channel features a web (the flat back section) with two flanges extending from it, but here's the key distinction—C-channels have flanges that may vary in thickness or feature tapered edges. According to industry classifications, there are three primary C-channel standards: Aluminum Association (with thicker walls and rounded inner corners), American Standard (with flanges that taper toward the top), and Canadian Standard. This open-sided design makes C-channels ideal for structural framing, vehicle chassis applications, racking systems, and store fixtures where you need accessible interior space.
The aluminum u channel, sometimes called a u shaped aluminum channel, has a more symmetrical profile with perpendicular flanges of uniform thickness. Think of it as a squared-off "U" shape. This geometry excels at edge protection, sliding track systems, glass panel framing, and architectural accents. With wall thicknesses typically ranging from 1/16 inch to 1/4 inch, these profiles accommodate diverse load requirements and design demands.
When should you choose one over the other? Select C-channels when your project demands higher load-bearing capacity or requires the structural standards common in construction framing. Choose U-channels when you need clean edge containment, sliding mechanisms, or a more finished aesthetic appearance.
Beyond the versatile C and U shapes, several specialty profiles address targeted needs that general-purpose channels simply cannot fulfill.
The aluminum hat channel, named for its hat-like cross-section with horizontal flanges, is engineered specifically for furring and leveling walls, ceilings, and exterior surfaces. What makes it special? This profile delivers an exceptional strength-to-weight ratio while efficiently supporting drywall, metal panels, plasterboard, and masonry. In commercial and residential construction, hat channels prove invaluable for their moisture resistance, fire protection properties, and ability to correct uneven surfaces.
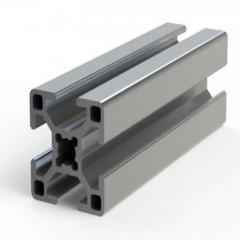
The aluminum t channel, particularly T-slot configurations, revolutionizes modular assembly. These profiles feature precision-engineered T-shaped slots that accept sliding T-nuts or specialized fasteners. Imagine building industrial machine frames, workstations, or automation equipment without welding or specialized clamping—that's the flexibility T-slot channels provide. Their adaptability supports rapid prototyping and lean manufacturing workflows where configurations need frequent adjustment.
The aluminum f channel resembles the letter F and shares similarities with U-channels but offers a unique extended web design without a second flange. This configuration provides flexibility for panel edge protection, transitions, partition framing, and window glazing applications, particularly in curtain wall systems and cabinetry.
J-channels have been essential in construction since the 1950s, primarily for vinyl siding installations and trim work. The distinct 90-degree bend creates a channel that mounts siding securely at corners and rooflines while providing weatherproof sealing. Additionally, the aluminum i channel (or I-beam) handles heavy-duty structural applications where exceptional loading and span distances are requirements.
| Profile Type | Cross-Section Shape Description | Primary Applications | Key Advantages |
|---|---|---|---|
| C-Channel | Web with two flanges; may have tapered edges or rounded corners | Structural framing, vehicle chassis, racking systems, construction | High load capacity, multiple industry standards available |
| U-Channel | Symmetrical U-shape with perpendicular uniform flanges | Edge protection, sliding tracks, glass framing, shelving | Clean aesthetics, versatile wall thickness options |
| Hat Channel | Hat-like profile with horizontal flanges extending from web | Wall furring, ceiling leveling, drywall mounting | Excellent strength-to-weight ratio, moisture resistant |
| T-Channel/T-Slot | T-shaped slots for fastener insertion | Modular frames, workstations, automation equipment | Tool-free assembly, infinitely adjustable |
| F-Channel | F-shaped with extended web, single flange | Panel mounting, transitions, window glazing | Flexible installation, clean edge finishing |
| J-Channel | 90-degree bent profile resembling letter J | Siding installation, trim work, exterior finishing | Weatherproof sealing, easy installation |
Understanding these geometric distinctions helps you match profile selection to project requirements rather than defaulting to whatever's readily available. As you'll discover in the next section, the alloy composition and temper designation of your chosen profile matters just as much as its shape.
You've selected the perfect profile shape—but here's where many projects go wrong. Choosing between a 6061 aluminum channel and a 6063 alternative isn't just about checking a box on a spec sheet. These alloy designations, along with their accompanying temper codes, fundamentally determine how your channel performs under stress, how easily it machines, and how long it resists corrosion. Let's decode what these numbers actually mean for your project.
Both 6061 and 6063 belong to the 6000 series aluminum family, containing magnesium and silicon as primary alloying elements. They look nearly identical and share similar base compositions. So why does the distinction matter? The devil lies in the details.
According to Metal Supermarkets, 6061 aluminum extrusion contains up to twice the iron content of 6063, along with higher levels of copper, chromium, and silicon. These additions translate directly into mechanical performance. On the Brinell hardness scale, 6061 scores approximately 95 compared to 6063's 73—a difference you'll feel when the channel bears structural loads.
When should you specify each alloy? Consider these key properties:
6061 Aluminum Properties:
6063 Aluminum Properties:
Here's a practical decision guide: if your 6061 channel needs to bear significant loads or undergo extensive machining, choose 6061. If appearance matters more than raw strength—think exposed architectural elements or furniture—6063 delivers that smooth, anodizable finish professionals prefer. Interestingly, for round tubing extrusions, 6063 actually provides higher product strength due to its superior extrudability in that specific configuration.
Sounds complex? The temper designation following the alloy number tells you exactly how the aluminum was heat-treated after extrusion. This processing history determines the material's final strength, and understanding it prevents costly specification errors.
The heat treatment process works like this: manufacturers raise the alloy temperature to approximately 980°F and hold it there for about an hour. This dissolves all alloying elements into a solid solution within the aluminum matrix. Rapid water quenching then locks these elements in place, preventing precipitation during cooling.
T5 Temper: When extrusions are quenched directly from the extrusion press while still hot, then artificially aged, the result is T5 material. This process is more economical since it skips the separate solution heat treatment step. T5 works well for applications where maximum strength isn't critical but good mechanical properties are still needed.
T6 Temper: For 6061 t6 ss (solution heat-treated and artificially aged) specifications, the material undergoes separate solution treatment, quenching, and then aging at temperatures between 325-400°F. During aging, alloying elements form ordered atomic arrays called GP zones that significantly strengthen the aluminum. Three common aging cycles achieve equivalent results: one hour at 400°F, five hours at 350°F, or eight hours at 325°F.
What does this mean practically? A 6061 t6 aluminum channel offers higher yield strength and fatigue resistance compared to T5 material of the same alloy. For structural applications governed by ASTM B308 standards—which cover aluminum alloy channels for general applications—T6 temper typically meets the most demanding requirements.
The temper choice also affects fabrication. Both T5 and T6 materials machine and weld well, but T6's higher hardness may require adjusted cutting parameters. For welding, remember that heat from the weld zone will soften the surrounding tempered material, potentially reducing local strength. Proper joint design accounts for this reality.
With alloy and temper fundamentals clear, your next consideration involves translating these specifications into the right dimensional parameters for your project.
You've selected your profile type and nailed down the alloy specification—now comes the question that trips up even experienced engineers: what size do you actually need? Reading aluminum channel sizes correctly prevents costly ordering mistakes and ensures proper fit-up during installation. Let's demystify the measurement conventions and standards that govern these specifications.
When you encounter aluminum channel dimensions on a spec sheet, you'll typically see a designation format like "4 x 2" or "CS 6 x 2.83." What do these numbers actually mean? The first number represents the channel depth (the height of the web), while the second indicates either flange width or weight per linear foot, depending on the standard being used.
According to the Aluminum Association Standards, channel specifications include several critical measurements:
Why does this matter? Imagine specifying a channel based solely on depth when your application actually requires specific flange width for mounting hardware. That oversight could mean rework or complete material replacement. Always verify all dimensional parameters—not just the headline numbers.
The relationship between wall thickness and load-bearing capacity follows predictable engineering principles. Thicker walls increase the moment of inertia and section modulus, directly improving bending resistance. For example, a 6 x 3 1/4 inch channel with 0.21-inch web thickness delivers a moment of inertia (Ix) of 21.0 in⁴, compared to just 14.4 in⁴ for the thinner 6 x 2 1/2 inch profile with 0.17-inch web thickness.
When reviewing an aluminum channel sizes chart, you'll notice alum channel sizes follow established patterns. Standard depths range from 2 inches for light-duty applications up to 12 inches for heavy structural work. Here's a practical reference showing common aluminum u channel dimensions and C-channel parameters:
| Size (in x in) | Depth (in) | Width (in) | Web Thickness (in) | Weight (lb/ft) | Sectional Area (in²) |
|---|---|---|---|---|---|
| 2 x 1 | 2 | 1.00 | 0.13 | 0.58 | 0.49 |
| 3 x 1 1/2 | 3 | 1.50 | 0.13 | 1.14 | 0.97 |
| 4 x 2 | 4 | 2.00 | 0.15 | 1.74 | 1.48 |
| 6 x 2 1/2 | 6 | 2.50 | 0.17 | 2.83 | 2.41 |
| 8 x 3 | 8 | 3.00 | 0.19 | 4.15 | 3.53 |
| 10 x 3 1/2 | 10 | 3.50 | 0.25 | 6.14 | 5.22 |
| 12 x 4 | 12 | 4.00 | 0.29 | 8.27 | 7.04 |
What about tolerances? According to ANSI H35.2 standards, aluminum c channel sizes and aluminum u channel sizes follow these general guidelines:
Tight tolerances beyond these standards are achievable but require discussion with your extruder. Expect modifications to dies, slower extrusion rates, increased inspection, and potentially higher rejection rates—all factors that increase cost. Standard tolerances meet most applications; specify tighter tolerances only when assembly fit-up genuinely demands it.
Several factors should influence your aluminum c channel dimensions and size selection:
With dimensional specifications clarified, your next decision involves selecting the right surface finish to protect your investment and achieve the desired aesthetic—a choice that significantly impacts both performance and longevity.
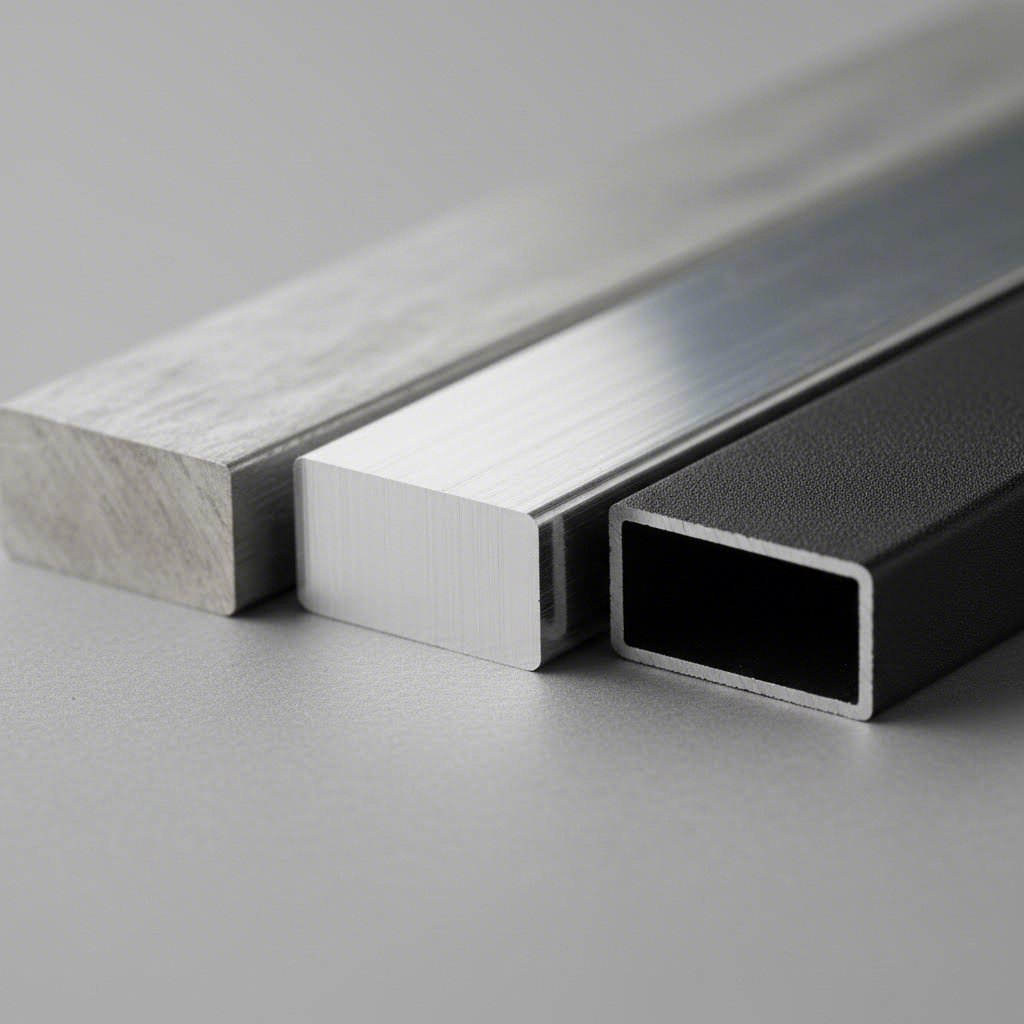
You've specified the perfect alloy, temper, and dimensions—but here's where aesthetics meets performance. The surface finish you select determines not just how your aluminum trim channel looks on day one, but how it performs years down the road. From cost-effective mill finishes to high-performance PVDF coatings, each option carries distinct trade-offs in durability, appearance, and budget. Let's explore what actually matters when making this decision.
When aluminum exits the extrusion die, it carries what manufacturers call a "mill finish." This raw state reflects the natural appearance of the metal—complete with die marks, slight oxidation, and a somewhat dull surface. According to Gabrian, mill finish is generally suitable only for products made as cheaply as possible, where appearance doesn't matter and short service life is acceptable.
Why would anyone choose mill finish? Cost savings, plain and simple. For aluminium trim channel hidden inside walls, behind panels, or in non-visible structural applications, paying for decorative finishing makes little sense. However, if your project involves any exposure to moisture, corrosive environments, or public view, you'll want something more robust.
Anodizing transforms the aluminum surface through an electrochemical process that grows the naturally occurring oxide layer into a much thicker protective barrier. Unlike paints or coatings applied externally, this aluminum oxide layer becomes integral to the metal itself—it cannot peel or flake. The Aluminum Association classifies anodizing thickness as Class I (0.7 mils) or Class II (0.4 mils), with coating life directly proportional to thickness.
When your project demands vibrant, long-lasting color with excellent UV resistance, powder coating emerges as a compelling option. This process electrostatically applies dry paint powder to prepared aluminum surfaces, by oven curing that melts and bonds the coating into an even finish. For a black aluminum u channel or any custom color application, powder coating delivers exceptional aesthetic flexibility.
According to Master Craft Finishers, advances in powder formulation now allow AAMA 2605-certified finishes with warranties reaching 20 to 30 years. This development places powder coatings on par with traditional PVDF paints in terms of durability.
For demanding architectural applications—think aluminium hat channel on exterior curtain walls or high-rise facades—PVDF coatings (commonly known by trade names Kynar or Hylar) represent the premium choice. These resin-based coatings have dominated the architectural market since 1965, offering exceptional color stability under prolonged UV exposure and chemical resistance that other finishes cannot match.
| Finish Type | Durability | Cost Level | Best Applications | Color Options |
|---|---|---|---|---|
| Mill Finish | Low | Lowest | Hidden structural components, temporary installations | Natural aluminum only |
| Anodizing (Class I) | High | Moderate | Storefronts, handrails, high-traffic areas | Limited (metallic tones, basic colors) |
| Powder Coating | High | Moderate | Interior/exterior trim, equipment frames, furniture | Extensive (hundreds of colors) |
| PVDF/Kynar | Very High | Highest | Curtain walls, metal roofing, exterior cladding | Extensive with superior fade resistance |
How do you choose? Match the finish to your environment and visibility requirements. Anodizing excels on storefronts and anywhere abrasion resistance matters most. Powder coating offers the best value for vibrant colors on interior and protected exterior applications. PVDF remains the gold standard for exposed architectural surfaces demanding decades of color stability. With surface treatment decisions clear, your next step involves understanding how these channels perform across different industry applications.
Now that you understand alloys, dimensions, and finishes, a practical question remains: where do these profiles actually get used? The answer spans nearly every industry imaginable. Aluminum channel applications extend far beyond simple framing—from the curtain walls of downtown skyscrapers to the extruded aluminum rails guiding automated manufacturing lines. Understanding sector-specific uses helps you recognize why this material dominates so many applications and how to leverage its properties for your particular project.
Walk into any modern commercial building, and you're surrounded by aluminum extrusion channel profiles—most of them invisible to the casual observer. According to Hydro Extrusion, extruded aluminum components resist distortion caused by weather and building movement, retaining strength and flexibility under loads while springing back from impact shock.
Why does construction rely so heavily on these profiles? Consider the demands: structures must withstand decades of thermal cycling, resist corrosion from rain and humidity, and maintain dimensional stability as buildings settle and shift. Aluminum channel track systems meet these requirements while offering installation simplicity that steel alternatives cannot match.
The construction sector particularly values aluminum's corrosion resistance. Unlike steel that demands continuous paint maintenance or galvanizing, aluminum naturally forms a protective oxide layer. This translates directly to reduced lifecycle costs—a factor that justifies aluminum's higher initial material cost in many architectural specifications.
Step onto a factory floor, and aluminum track systems guide everything from conveyor components to robotic arms. The manufacturing sector has embraced these profiles for their modularity, precision, and the ability to reconfigure production lines without extensive rework.
What makes aluminum channel ideal for industrial settings? The answer lies in the combination of strength-to-weight ratio and dimensional consistency. When mounting sensors, cameras, and actuators on automation systems, engineers need profiles that hold tight tolerances while allowing positional adjustments during setup. T-slot aluminum channels deliver exactly this capability.
The modularity factor deserves special emphasis. Unlike welded steel structures that require cutting and re-fabrication for changes, T-slot aluminum systems allow complete disassembly and reconfiguration. For lean manufacturing environments where flexibility drives competitiveness, this adaptability proves invaluable.
Open any electronic enclosure, and you'll likely find aluminum channels serving critical functions. The technology sector relies on these profiles for reasons beyond simple structure—thermal management and electromagnetic considerations drive material selection.
Aluminum conducts heat efficiently, making it ideal for automobile radiators, air conditioners, nuclear reactors, and computing equipment. When processors generate heat that must dissipate quickly, extruded aluminum heat sinks provide the surface area and thermal conductivity required. Additionally, extruded aluminum tubing houses coaxial cables and wires because it's non-magnetic—useful for high-voltage applications and around sensitive magnetic devices.
The electronics industry particularly appreciates aluminum's electromagnetic shielding properties. Properly designed enclosures block radio frequency interference that could disrupt sensitive circuits or violate regulatory emission limits. This dual functionality—structure plus shielding—makes aluminum channel the default choice for countless electronic products.
Every pound saved in vehicle construction translates to improved fuel efficiency and performance. This fundamental equation explains why transportation manufacturers have aggressively adopted aluminum extrusion channels across vehicle types—from passenger cars to commercial trailers.
According to industry sources, demand has grown significantly for aluminum extrusions as structural components in lighter-weight automobiles, exemplified by vehicles like the Ford F-150 pickup truck that shed 700 pounds through aluminum construction. The strength-to-weight ratio that makes aluminum attractive for aircraft applies equally to ground vehicles.
Beyond weight savings, transportation applications demand materials that endure vibration, thermal cycling, and sometimes harsh environments. Aluminum extrusion channels deliver on all counts—particularly when proper alloy selection (typically 6061-T6 for structural applications) matches the specific loading conditions.
Understanding these sector-specific applications reveals a pattern: aluminum extrusion channel succeeds wherever weight reduction, corrosion resistance, thermal management, or assembly flexibility matters. With application context established, the next logical question becomes how to actually work with these profiles during fabrication and installation.
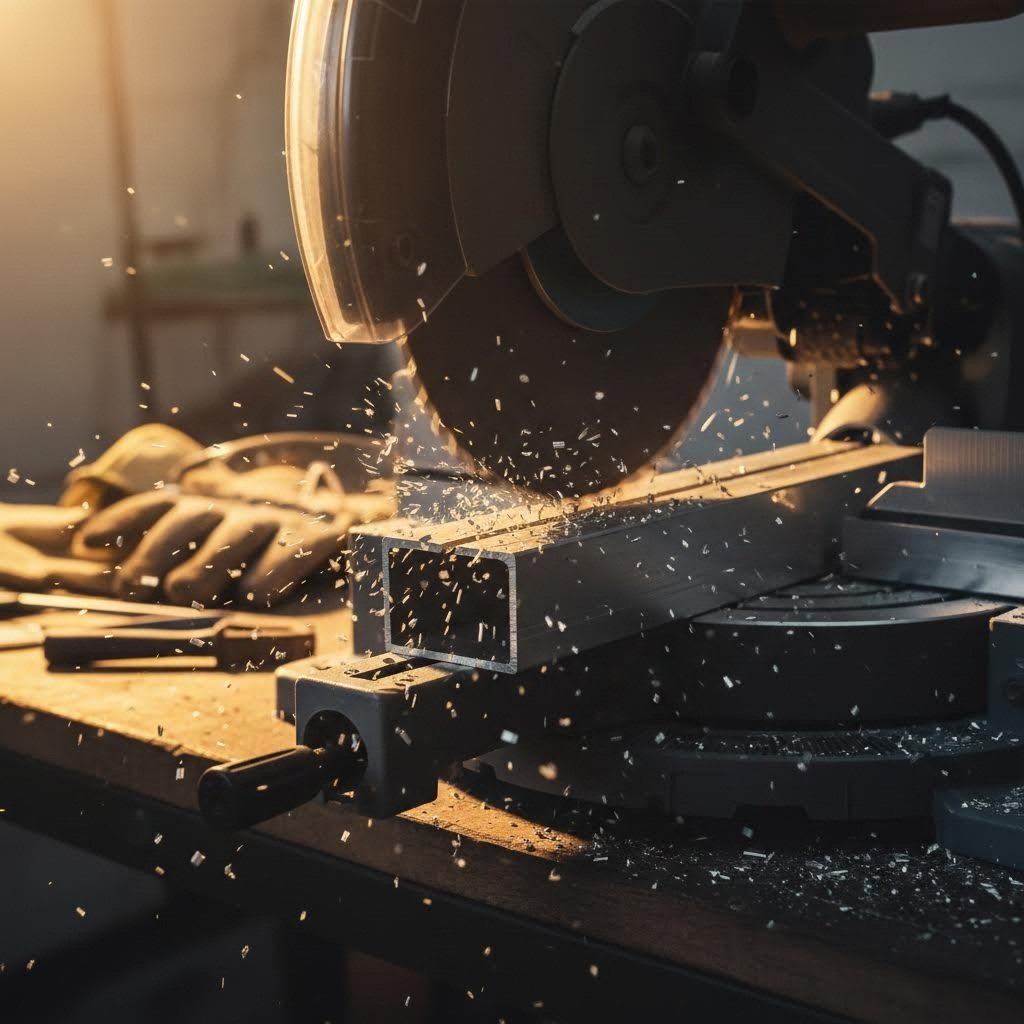
So you've specified the perfect profile, selected your alloy, and the material has arrived at your shop. Now what? Working with aluminum channels requires different techniques than steel or other metals—and getting it wrong means wasted material, poor fit-up, and frustrating rework. Whether you're cutting a single extruded aluminum c channel for a weekend project or fabricating hundreds of pieces for a commercial installation, these practical guidelines help you achieve professional results.
Aluminum is a soft metal, which sounds like good news until you realize this characteristic creates its own challenges. According to Industrial Metal Service, anyone who has tried to weld up a strict ninety-degree angle on aluminum knows that pieces coming off a chop saw are always a degree or two off. Understanding why this happens—and how to prevent it—separates amateur cuts from professional results.
The most common cutting problems include curved cuts from blade flex under pressure, angled edges when blades curve through the material thickness, and chipping or burrs where soft aluminum fails to separate cleanly. These flaws might seem minor on a single piece, but they compound quickly across large projects where hundreds of aluminum channels need precise fit-up.
What tools should you have ready? Your equipment choices directly impact cut quality:
Drilling and tapping aluminum u-channel requires attention to different factors. Use sharp high-speed steel or cobalt drill bits with 118-135 degree point angles. Apply cutting fluid liberally—aluminum tends to gall and stick to tooling without proper lubrication. For tapping, specify roll-form taps rather than cutting taps when possible; they create stronger threads by displacing rather than removing material.
What about bending? Here's where alloy and temper selection becomes critical. Annealed aluminum (O temper) bends easily but lacks strength. T6 temper material offers maximum strength but minimum ductility—aggressive bending causes cracking. For channel frame applications requiring formed shapes, consider specifying T4 temper material and heat-treating to T6 after forming, or design joints that avoid bending altogether.
Connecting aluminum channels offers multiple options, each suited to different performance requirements and skill levels. Mechanical fasteners provide the simplest approach—bolts, screws, and rivets require no special equipment beyond basic hand tools. For channel rail assemblies and modular structures, T-slot connections allow tool-free adjustment and reconfiguration.
When should you choose welding instead? According to Amardeep Steel Centre, welding aluminum follows different rules than steel, with success depending on managing surface oxide, high thermal conductivity, hydrogen absorption risks, and subtle melting cues. TIG welding (GTAW) delivers top quality and control for precision work, while MIG welding (GMAW) offers faster deposition rates for production applications.
Mechanical Fastening Considerations:
Welding Considerations by Alloy:
The most common fabrication mistakes? Skipping surface preparation tops the list. Aluminum's natural oxide layer must be removed immediately before welding—wire brush the joint, then weld within minutes. Using steel wire brushes contaminates the aluminum, so dedicate stainless steel brushes exclusively for aluminum work. Inadequate clamping ranks second; aluminum's high thermal conductivity means heat spreads rapidly, causing distortion if parts aren't properly fixtured.
For critical structural connections, consider adhesive bonding combined with mechanical fasteners. Modern structural adhesives designed for aluminum achieve remarkable strength while distributing stress across the entire joint area rather than concentrating it at fastener holes. This hybrid approach proves particularly effective for thin-wall aluminum channels where drilling would unacceptably weaken the profile.
With fabrication fundamentals covered, you might wonder how aluminum compares to alternative materials for your specific application—a comparison that often reveals surprising trade-offs.
You've mastered fabrication techniques and understand application requirements—but here's a question that deserves honest consideration: is aluminum actually the right material for your project? While aluminum extrusion channels dominate many applications, steel, stainless steel, and even plastic alternatives each offer compelling advantages in specific scenarios. Making an informed choice requires understanding exactly where each material excels and where it falls short.
The c channel metal debate often comes down to aluminum versus steel—and the answer isn't as straightforward as you might expect. According to Shielden, steel is roughly three times denser than aluminum (7.8 g/cm³ versus 2.7 g/cm³), which means a one-meter length of standard 1-5/8 inch steel channel weighs approximately 4.0 kg compared to just 1.4 kg for the aluminum equivalent.
What does this weight difference mean practically? When you're installing overhead electrical conduit or building lightweight support systems, alum channel offers easier handling—often allowing single-person installation where steel would require two workers or mechanical assistance. For c channel framing in transportation applications, every pound saved translates directly to improved fuel efficiency and increased payload capacity.
However, steel delivers significantly higher absolute strength and stiffness. Steel strut channels excel in long-span installations, heavy conduit racks, and dynamic load environments where vibrating equipment demands rigid support. If your project involves industrial machinery bases or applications requiring minimal deflection under heavy loads, steel's inherent stiffness often justifies the weight penalty.
Corrosion resistance creates another clear distinction. Aluminum naturally forms a protective oxide layer that resists corrosion without additional treatment—a major advantage in coastal installations or environments exposed to moisture. Steel requires protective coatings like galvanizing or powder coating to prevent rust, adding both initial cost and ongoing maintenance requirements. For alum c channel applications in outdoor or humid environments, this inherent protection proves invaluable.
Cost considerations favor steel initially. Raw steel typically costs less per pound than aluminum, making it attractive for budget-conscious projects where weight isn't critical. However, when you factor in coating requirements, maintenance needs, and the total installed cost including labor for heavier materials, the economic picture becomes more nuanced.
Stainless steel occupies a middle ground that deserves careful consideration. According to Haina Solar, stainless steel offers superior corrosion resistance in marine environments and chemical exposure scenarios where even aluminum might struggle. The 316 stainless grade handles saltwater conditions exceptionally well—making it the preferred choice for marine applications despite its higher cost.
When does stainless steel make sense over aluminum structural shapes? Consider stainless for heavy-duty applications requiring both corrosion resistance and maximum strength, such as chemical processing equipment, food manufacturing facilities, or structures exposed to aggressive cleaning chemicals. Stainless also welds more predictably using standard MIG and TIG techniques, whereas aluminum welding demands specialized skills and equipment.
Plastic channels—typically PVC, fiberglass, or composite materials—enter the conversation for specialized applications. These materials offer complete corrosion immunity, electrical insulation, and often lower weight than even aluminum. However, plastic c chanel alternatives sacrifice strength, temperature resistance, and long-term dimensional stability. For electrical conduit protection in corrosive environments or applications requiring non-conductive properties, plastic alternatives merit evaluation.
| Property | Aluminum | Carbon Steel | Stainless Steel | Plastic/Composite |
|---|---|---|---|---|
| Weight (Relative) | Low (1x) | High (3x) | High (3x) | Very Low (0.5x) |
| Corrosion Resistance | Excellent (natural oxide) | Poor (requires coating) | Excellent | Excellent |
| Strength-to-Weight Ratio | Excellent | Good | Good | Fair |
| Absolute Strength | Moderate | High | High | Low |
| Initial Material Cost | Moderate | Low | High | Low to Moderate |
| Maintenance Cost | Low | Moderate to High | Low | Low |
| Temperature Resistance | Good (to ~400°F) | Excellent | Excellent | Poor (limited) |
| Best Applications | Architectural, transportation, electronics, modular framing | Heavy machinery, long spans, industrial structures | Marine, chemical processing, food equipment | Non-conductive, highly corrosive environments |
So when is aluminum the optimal choice? Select alum channel when weight reduction matters—whether for easier installation, improved vehicle efficiency, or reduced structural loading. Choose aluminum when corrosion resistance must come without ongoing maintenance. And prioritize aluminum when you need complex extruded profiles that steel cannot economically match.
When should you consider alternatives? Steel wins for maximum strength at minimum cost in protected environments. Stainless steel excels in extreme corrosion scenarios demanding high load capacity. Plastic serves niche applications requiring electrical insulation or chemical immunity. Understanding these trade-offs empowers you to specify the right material rather than defaulting to familiar options.
With material selection clarified, your final decisions involve choosing between standard catalog profiles and custom extrusions—a choice that balances economics against project-specific requirements.
You've compared materials, mastered fabrication techniques, and understand exactly what your project demands. Now comes a decision that directly impacts both your budget and timeline: should you specify standard catalog profiles or invest in custom extrusion tooling? This choice involves more complexity than simply checking prices—you're weighing upfront tooling costs against long-term value, lead times against design optimization, and supplier capabilities against project requirements. Let's break down the economics and evaluation criteria that guide this decision.
When you need an aluminum track channel or basic structural profile, standard options often make perfect sense. According to industry data, standard aluminum profiles typically cost 30% to 50% less than custom alternatives. Manufacturers produce these shapes in large quantities using existing dies, which eliminates tooling charges and enables immediate availability.
Why would anyone pay more for custom profiles? The answer lies in optimization. When your u channel aluminum extrusion requires specific internal features, non-standard dimensions, or integrated mounting points, custom dies become worthwhile investments. Custom profiles can incorporate T-slots, screw ports, or complex geometries that eliminate secondary operations—turning what would require multiple standard profiles and extensive fabrication into a single extruded component.
Consider these aluminum channel specifications when evaluating the standard versus custom question:
The tooling investment deserves careful analysis. According to extrusion industry sources, die costs vary significantly based on complexity:
| Profile Complexity | Typical Die Cost | Lead Time for Die |
|---|---|---|
| Solid profile dies | $1,250 | 10-15 days |
| Hollow dies | $1,950 | 15-20 days |
| Complex or multi-hollow dies | Up to $5,000 | 15-20 days |
Here's where order volume transforms the equation. For a $2,000 die producing 500 meters of c channel aluminum extrusion, the tooling adds $4 per meter to your cost. Increase that order to 5,000 meters, and tooling contribution drops to just $0.40 per meter—often making custom profiles competitive with or even cheaper than standard alternatives requiring extensive post-processing.
Lead times also factor into your decision. Standard profiles typically ship within 7 to 14 days since aluminum channel suppliers maintain inventory. Custom u channel aluminium extrusion projects require 15 to 30 days total—including die manufacturing, extrusion production, and any surface finishing. For time-critical projects, standard profiles offer obvious advantages; for planned production runs, the additional lead time rarely creates problems.
Whether you're sourcing standard extruded aluminum u channel or commissioning custom aluminum channel types, supplier capability directly determines project success. A supplier with inadequate equipment, weak quality systems, or poor communication creates risks that no price advantage can justify.
What should you evaluate when selecting aluminum channel suppliers? According to procurement specialists, press capacity represents the starting point. Small presses (600-1800T) produce thin, precise profiles; medium presses (2000-3500T) handle general industrial work; large presses (5000-10,000T) create heavy structural components. A supplier with multiple press capacities offers flexibility as your requirements evolve.
For projects requiring comprehensive custom capabilities, suppliers with extensive equipment fleets demonstrate production flexibility. Shengxin Aluminium, for example, operates 35 extrusion presses ranging from 600T to 5500T, supported by CNC machining centers capable of precise cutting, drilling, and bending. This range means a single supplier can handle everything from delicate architectural trim to heavy structural components—providing end-to-end support from die development through mass production. Their custom aluminum extrusion services exemplify what integrated capability looks like in practice.
Quality systems deserve particular scrutiny. According to industry benchmarks, professional suppliers should provide:
The decision between standard and custom profiles ultimately depends on matching your project's specific requirements against total lifecycle cost—not just initial material price. Standard profiles from reliable aluminum channel suppliers work perfectly for straightforward applications. Custom extrusions shine when design optimization, reduced assembly complexity, or precise performance requirements justify the tooling investment. With supplier evaluation criteria clear, your final step involves synthesizing all these considerations into confident specification decisions.
You've absorbed a tremendous amount of information—from alloy chemistry to fabrication techniques, from profile geometries to supplier evaluation criteria. But knowledge without action doesn't move your project forward. How do you synthesize everything you've learned into confident purchasing decisions? The answer lies in systematically matching specifications to your actual application requirements rather than defaulting to whatever's readily available or cheapest on paper.
Think of channel aluminum selection like solving a puzzle. Each piece—profile type, alloy grade, temper designation, dimensions, and surface finish—must interlock with the others while fitting your project's unique constraints. Get one piece wrong, and the entire assembly suffers. Get them all right, and you've built something that performs reliably for years.
Before contacting suppliers or placing orders, work through these prioritized decisions. Each step builds on the previous ones, creating a specification package that communicates exactly what you need.
What separates successful projects from frustrating ones? Typically, it's the discipline to complete this checklist before requesting quotes. Suppliers can provide accurate pricing only when specifications are clear. Vague requirements lead to conservative (expensive) quotes or, worse, materials that don't meet your actual needs.
With your specifications defined, you're ready to engage suppliers productively. For standard aluminium u channel profiles and common configurations, multiple distributors likely stock what you need for quick delivery. Compare availability, pricing, and minimum order quantities across several sources.
For projects requiring custom aluminum extrusions, precision machining, or specialized surface treatments, supplier selection becomes more critical. Look for partners offering integrated capabilities—die design through finished product—rather than coordinating between multiple vendors. This integration reduces communication errors, eliminates handling damage between facilities, and typically accelerates delivery.
When your project demands comprehensive aluminum solutions, working with an experienced manufacturer makes all the difference. Shengxin Aluminium brings over 30 years of extrusion expertise to projects requiring precision deep processing. Their facility houses 35 extrusion presses spanning 600T to 5500T capacity, supported by CNC machining centers for precise cutting, drilling, and bending operations. Surface treatment capabilities include anodizing in custom colors like champagne and rose gold, powder coating, PVDF coatings for architectural durability, and micro-arc oxidation for superior hardness. Factory-direct pricing eliminates middleman markups while maintaining the quality control that comes from integrated production.
Whether you're sourcing standard aluminum c channels for a straightforward framing project or commissioning custom profiles with complex geometries and demanding tolerances, the principles remain consistent: match specifications to requirements, verify supplier capability, and consider total value rather than just initial price. Your investment in understanding these aluminum extrusion fundamentals pays dividends every time you specify materials correctly the first time—eliminating costly rework, reducing project delays, and delivering results that perform as expected for years to come.
Aluminum extruded channels are structural components created by forcing heated aluminum billets through specially designed dies at temperatures around 800-925°F. This process produces continuous profiles with uniform cross-sections in shapes like C, U, T, J, and hat channels. Each shape serves specific purposes—C-channels excel in structural framing, U-channels work for edge protection and sliding mechanisms, while T-slot channels enable modular assembly systems. The extrusion method delivers superior dimensional consistency compared to rolled or formed alternatives, making these profiles ideal for construction, manufacturing, electronics, and transportation applications.
C-channels feature a web with two flanges that may have tapered edges or rounded corners, following Aluminum Association, American Standard, or Canadian Standard specifications. They're designed for heavy structural applications like support beams, equipment frames, and vehicle chassis. U-channels have a more symmetrical profile with perpendicular flanges of uniform thickness, creating a squared-off shape. This geometry makes them ideal for edge protection, sliding track systems, glass panel framing, and architectural accents. Choose C-channels when load-bearing capacity is critical; select U-channels when you need clean edge containment or sliding mechanisms.
6061 aluminum channel is a U-shaped profile made from 6061 alloy, which contains magnesium and silicon with higher levels of iron, copper, and chromium than 6063. This composition provides superior strength, making it ideal for structural applications like braces, frames, trailers, and aerospace components. With a Brinell hardness of approximately 95, 6061 offers excellent machinability and weldability. The T6 temper designation indicates solution heat treatment and artificial aging for maximum strength. While 6063 provides better surface finish for architectural applications, 6061-T6 channels are preferred when mechanical performance and load-bearing capacity are primary concerns.
Aluminum channels have higher initial material costs compared to steel alternatives, though lifecycle costs often balance out due to lower maintenance requirements. They offer lower absolute strength than steel, making them unsuitable for extremely heavy loads or long unsupported spans. Welding aluminum requires specialized skills and equipment, as the heat-affected zone loses temper strength. Additionally, while aluminum resists general corrosion, it can experience galvanic corrosion when in contact with dissimilar metals without proper isolation. Temperature limitations exist too—aluminum loses strength above 400°F, unlike steel which handles higher temperatures effectively.
Standard profiles cost 30-50% less than custom alternatives and ship within 7-14 days since suppliers maintain inventory. Choose standard when basic structural or framing needs don't require specific internal features. Custom extrusions become worthwhile when your design requires non-standard dimensions, integrated mounting points, or T-slots that eliminate secondary operations. Die costs range from $1,250 for solid profiles to $5,000 for complex multi-hollow designs, with 15-30 day lead times. For larger orders, tooling costs spread across more units—at 5,000 meters, a $2,000 die adds only $0.40 per meter, often making custom profiles competitive with heavily fabricated standard alternatives.


 Onlineservice
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 Deutsch
 English
 français
 русский
 español
 português
 العربية
 ไทย
 Việt
 Українська